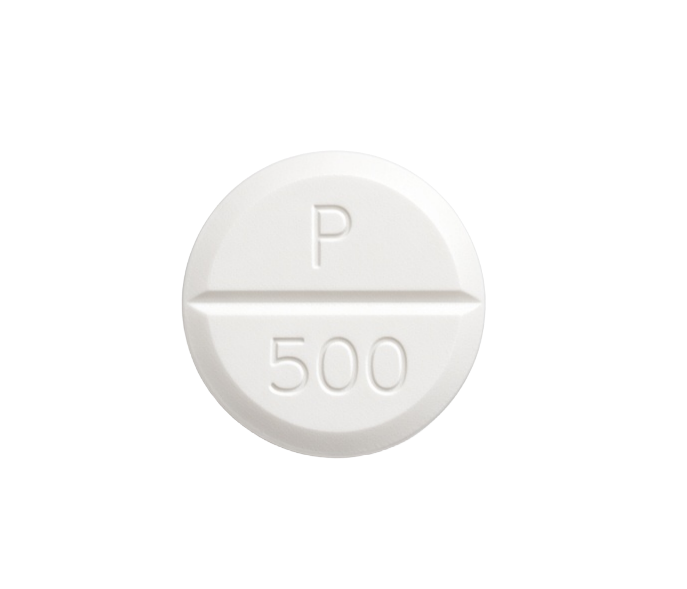
Tablets
Evaluate size, shape, color and visible appearance against the selected product recipe.
Inspect tablets, capsules and softgels directly on bottle-filling lines. A camera array, dedicated lighting and AI Deep Learning with Pattern Recognition synchronize inspection with slat movement. For pharmaceutical and nutraceutical production, including dietary supplements.
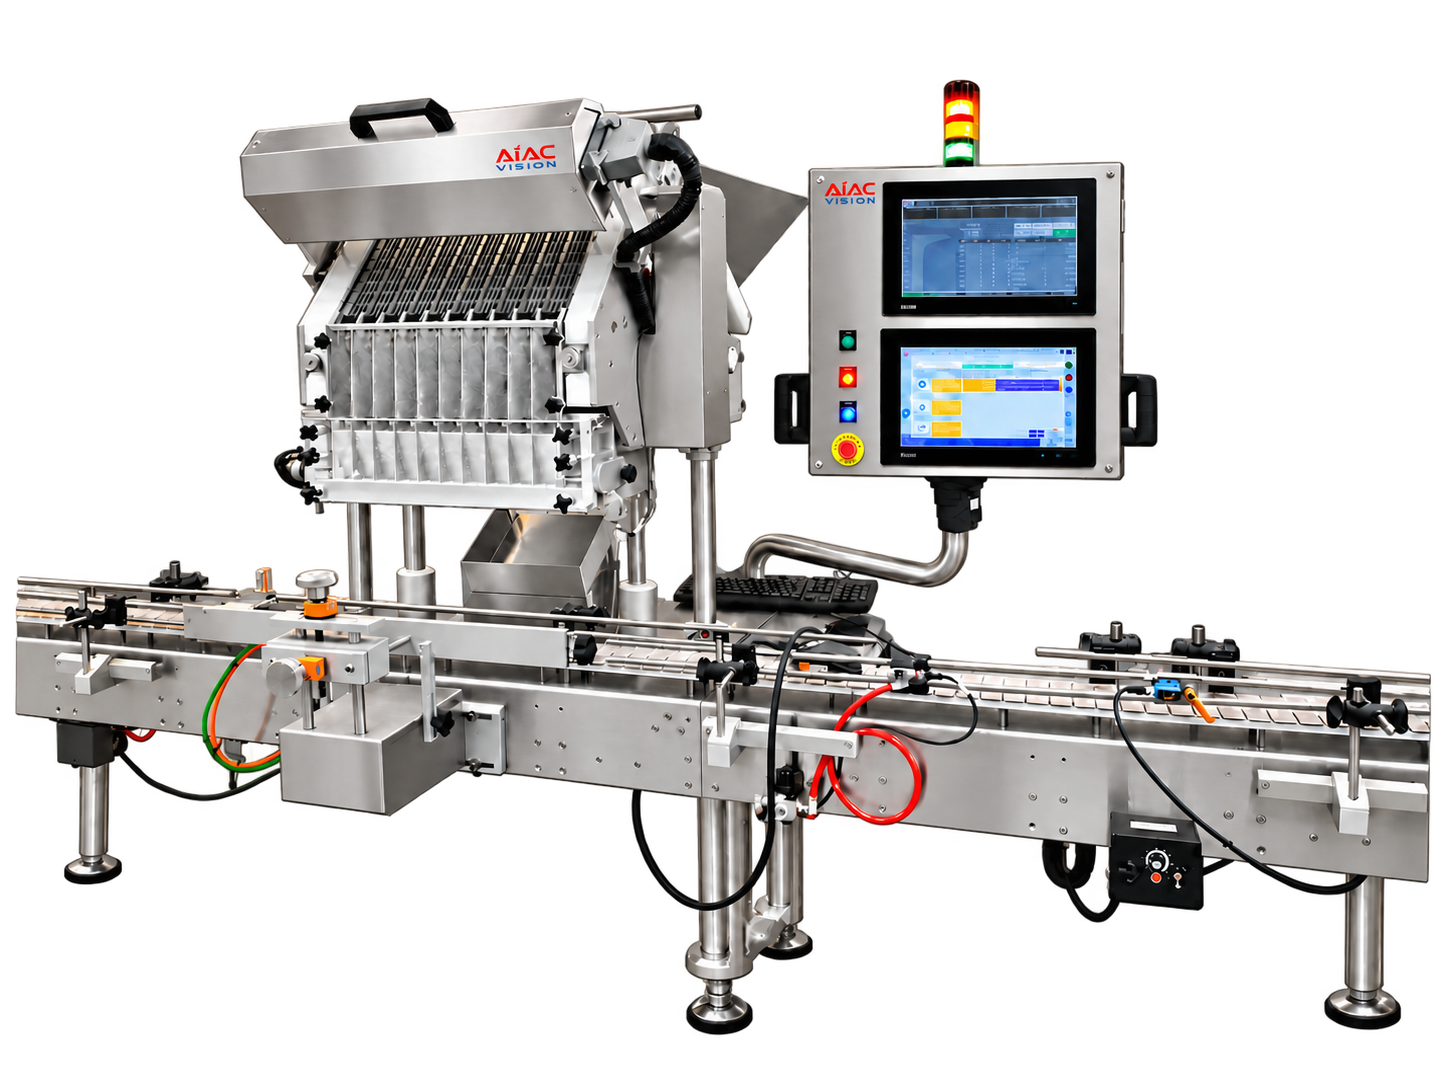
Slat counter vision inspection case study.
Product-specific recipes evaluate the surfaces visible to the camera array during inline handling.
Evaluate size, shape, color and visible appearance against the selected product recipe.
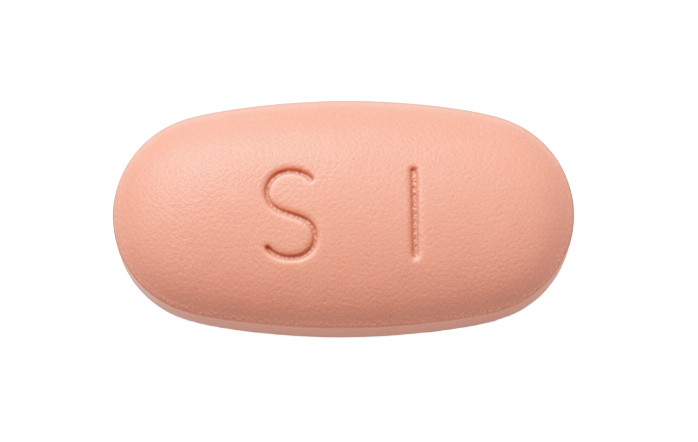
Evaluate size, shape, color and visible appearance against the selected product recipe.
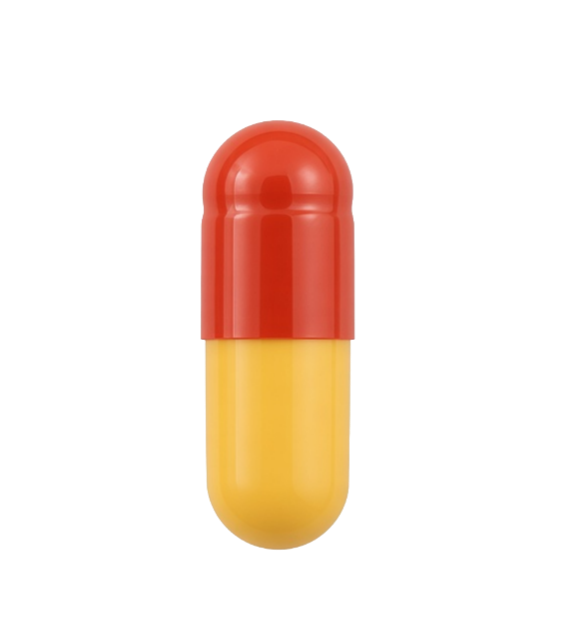
Evaluate size, shape, color and visible appearance against the selected product recipe.
Check broken or chipped products, abnormal size and shape, color deviations and visually distinguishable product mix-ups. Empty slat positions can also be identified.
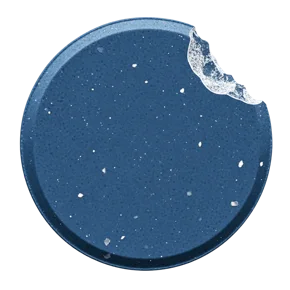
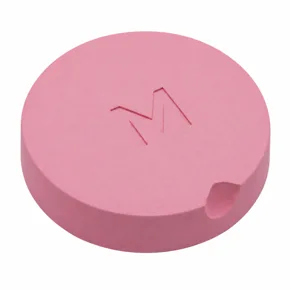
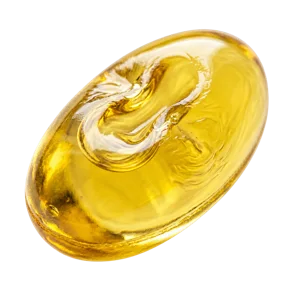
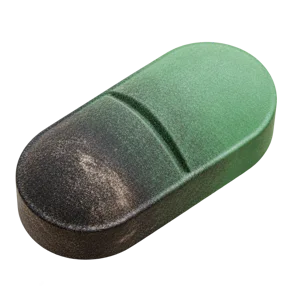
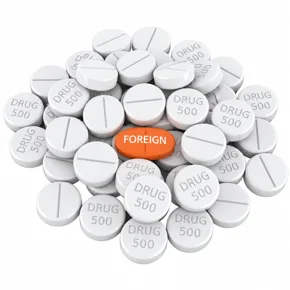
Representative appearance examples. Detectability depends on camera-visible surfaces, product presentation, lighting and the selected recipe.
A host-specific camera array and dedicated lighting capture the products as each slat passes the inspection position.
AI models and defined measurements check broken products, size, shape, color and empty positions.
Results are synchronized with the host controls and the agreed handling or rejection architecture.
Combine trained AI models with defined measurements for product-specific inspection.
Saved recipes and adjustable inspection parameters simplify setup and changeover.
Four user levels, defect statistics, PDF reports, audit trails and USB export support controlled operation and quality review.
Compare 15, 20 and 40 inch configurations.
| Slat width | 15 in |
|---|---|
| Capacity | Up to 28,800 slats/hour (8 slats/second) |
| Inspectable products | Tablets, capsules and softgels |
| Inspection contents | Broken, shape and color defects; empty slat positions |
| Number of cameras | 3 |
| Power | 1.5 kW |
| Power supply | 120/208 V AC, 60 Hz, 3-phase, 5-wire |
| Air pressure | 0.6 MPa |
| Air consumption | 4 gal/min |
| Dimensions, L × W × H | 27.8 × 11.0 × 15.1 in |
| Total weight | 65 lb |
Final performance depends on host-machine motion, presentation, product density, optical access and reject architecture.
Coordinate imaging, product tracking, rejection and bottle-filling controls around the host equipment.
Inspection is synchronized with slat movement. The host line coordinates the handling of rejected product and short-count bottles; counting accuracy and bottle control must be assessed with the host system.
The camera array, lighting and inspection timing are matched to the host slat counter.
The line coordinates rejected product and short-count bottle handling. Confirm the host machine rejection arrangement for the installation.
Provide the host model, slat dimensions, product, throughput and bottle handling requirements.
Share your product type, target defects and required capacity. We will help you evaluate the next step.